Sulzer PyroCon™: rapid quenching technology powering pyrolysis oil purification
Updated: Oct 1

Introduction
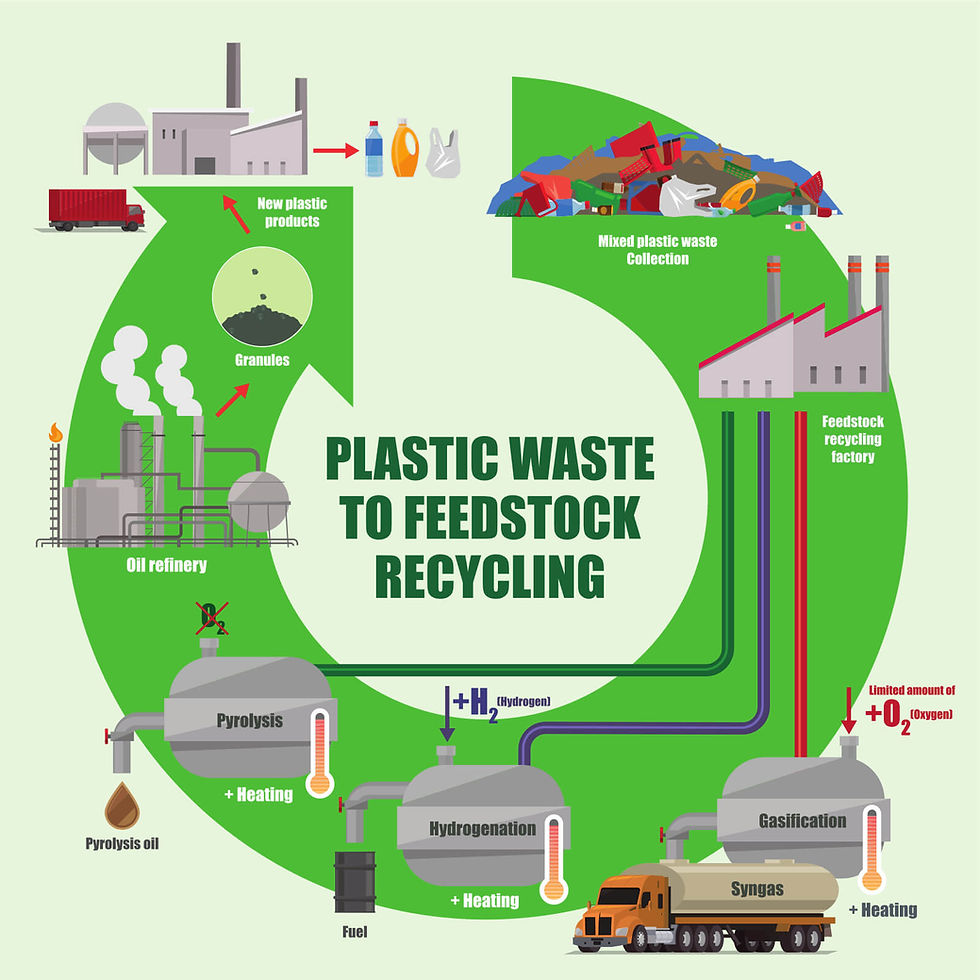
One of the critical hurdles in advanced plastic recycling via pyrolysis is efficient quenching the fast cooling of hot pyrolysis vapors to prevent secondary reactions and degradation. Sulzer’s PyroCon™ technology delivers breakthrough rapid condensation and anti-fouling design, boosting both product quality and process reliability.
How PyroCon™ technology works
Ultra-Fast Quenching:
PyroCon™ rapidly cools pyrolysis gases immediately after they’re generated, halting unwanted chemical reactions and protecting product integrity.
Anti-Fouling & Extended Uptime:
Innovative internal designs and liquid recirculation prevent solid build-up, dramatically reducing maintenance and downtime.
Flexible Construction:
The use of standard stainless steels allows for cost-efficient installation and operation, even under high-temperature pyrolysis conditions (up to 600°C).
Key benefits of Sulzer PyroCon™
Feature | Benefit |
Rapid vapor quenching | Maximizes recovery of valuable oil; limits by-products |
Anti-fouling design | Less unplanned shutdown, lower maintenance costs |
Higher process yields | More oil and hydrocarbons for downstream purification |
Modular and scalable | Deploys easily in both new and existing plants |
Industry-proven results | Operating at leading facilities (Quantafuel, Indaver, Carboliq) |
Multi-feed compatibility | Handles polyolefins, polystyrene, PMMA, bio-wastes |
Applications and performance
Plastics Processed:
Handles tricky feeds, such as PE, PP, PS, PMMA, and contaminated streams, as well as biomass residues.
Commercial Success:
PyroCon™ is installed at top European pyrolysis plants, delivering higher yields and less downtime compared to conventional quenching systems.
Why PyroCon™ sets a new standard
Reduced Product Degradation:
By stopping undesirable reactions instantly, PyroCon™ ensures the final pyrolysis oil is of higher quality more suitable for further purification into naphtha, diesel, aromatics, and other valuable products.
Supports a Circular Economy:
Enhances the viability and profitability of advanced recycling processes, helping divert plastic and biomass waste from landfills and fossil-based production.
Example process flow
Hot plastic and/or biomass vapors exit the pyrolysis reactor.
PyroCon™ chamber instantly quenches the vapors, condensing them into liquids while minimizing solids and by-products.
Stabilized liquid hydrocarbons move on for purification (e.g., removal of sulfur, chlorine, and further distillation).
Conclusion
Sulzer’s PyroCon™ is a game-changer for anyone purifying pyrolysis oil from mixed plastic or biomass waste. It delivers superior oil yields, cleaner product quality, and robust, low-maintenance performance empowering the next generation of advanced recycling and circular economy initiatives.